
CNC press brake forming · Gilbert
CNC Bending and Forming for Gilbert
Press-brake formed mounting brackets, channels and cover parts for Gilbert equipment enclosures, made to drawing in Phoenix.
Formed Channels and Brackets That Preserve Access
For a formed bracket beside AC or pool equipment, mark the finished envelope and any clearance needed for a removable panel or service opening. Show bend direction, inside dimensions, hole locations and handed versions. Those details let the forming review address the actual component rather than assume a standard angle.
Include the finished drawing alongside the flat pattern and identify the visible face and finish. KorFab reviews bend feasibility against the material, thickness and tooling. The enclosure layout, equipment clearances and installation remain with the buyer; this is component fabrication rather than a complete enclosure design service.

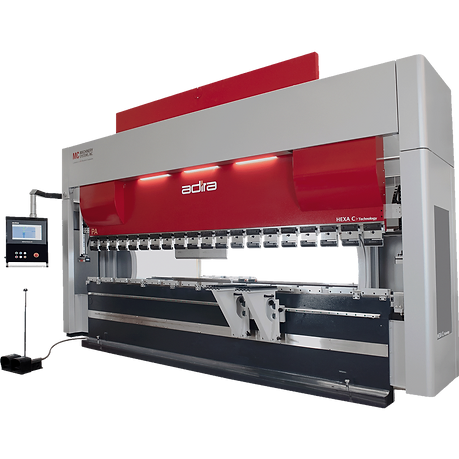
- Press force 135 metric tons (approx. 149 US tons)
- Bend length 3,000 mm (118 in), 2,550 mm (100.4 in) between frames
- Synchronized rams, CNC crowning and CNC backgauge
- Steel, stainless steel and aluminum
Bends that repeat across the run
You order parts that fit together on the bench, not parts that have to be pushed into place. Ram position, backgauge and crowning are set once and repeated for every piece, so a multi-bend part holds its sequence from the first article to the last.
- Press force
- 135 tPress force
- Bend length
- 3,000 mmBend length
- Between frames
- 2,550 mmBetween frames
Forming is planned with the cutting and welding around it, not quoted as a standalone operation.

The materials we form
Blanks in the common fabrication grades are formed on the press brake.
- Carbon steel
- Stainless steel
- Aluminum
- Light gauge sheet through plate
- Blanks cut here or supplied by you
- Bend details confirmed per part at quote
Send the material, thickness and bend detail. Anything beyond the brake is quoted on another machine rather than guessed at.
The machine that runs the work
- Machine
- CNC hydraulic press brake
- Press force
- 135 metric tons (approx. 149 US tons)
- Bend length
- 3,000 mm (118 in), 2,550 mm (100.4 in) between frames
- Control
- Synchronized rams, CNC crowning and CNC backgauge
- Materials
- Steel, stainless steel, aluminum
Figures are the manufacturer’s published specifications for the installed machine. Full breakdown: Mitsubishi ADIRA PA 13530.

Request a quote for your next project
Send the drawings, quantities and requirements for your Gilbert components.
Industries We Serve
The same formed part shows up differently by sector. These are the industries we fabricate for and what the work looks like in each.
Commercial Construction
Bent connection parts, supports and formed flashings taken from the project drawings.
Commercial constructionIndustrial Operations
Guards, covers and formed housings for machinery and plant equipment.
Industrial plants and equipmentManufacturing and OEMs
Formed brackets, channels and enclosure parts produced to print in batches.
Manufacturing and OEMsData Centers
Formed mounting brackets, covers and enclosure parts for equipment rooms.
Data centers
Metal Bending and Forming by city
Quote Your Gilbert Components
Send the finished drawing, flat pattern if available, bend angles, material, thickness, handed quantities and finish. Forming is in Phoenix and Gilbert delivery is agreed with the order.
Fabricated in Phoenix, Arizona, for Gilbert projects. Delivery is reviewed for each order; see delivery.